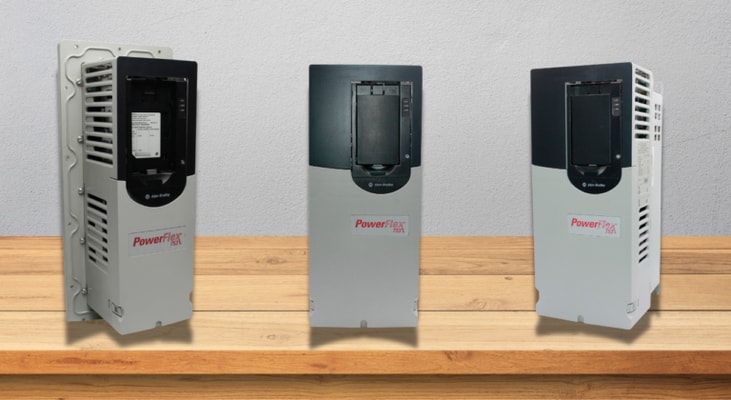
For many facilities, uptime is a priority when selecting which equipment to deploy in their line. Because of this, redundancy modules and spares are kept so that high-priority equipment and processes can be repaired with minimal downtime. As you can imagine, this is an effective technique when properly executed. Sometimes these processes are designed so well that they simply chug along for years and years without having to dust off the replacement in the supply cabinet. Drives that have been obtained for replacement now sit on the shelf waiting for the baton to be passed, and it can be years before it does, and plugging them in might just bring more issues. When it comes to storing drives, there is no official expiration date printed on the part, but guidelines for the amount of time a drive can sit without power. This time frame varies across manufacturers: Rockwell’s PowerFlex guidelines specify 2 years, while ABB and Eaton specify 1 year. This is because the electrolytic capacitors...
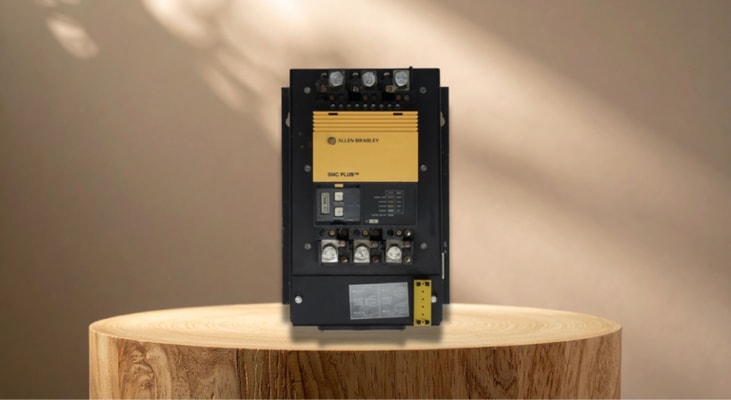
In the modern age, motor control isn’t as simple as it looks. There’s matching nameplate specifications, determining if the load you’re driving needs certain features like regeneration, or even figuring out if it’s worth futureproofing. With VFDs being so common today, it is easy to assume they are always the better answer. But that’s not always the case. Sometimes, less really is more. If the application only calls for smooth starting and stopping, a soft starter could be the cheapest, simplest, and most cost-effective choice. A soft starter, as the name implies, is a motor controller that gradually and smoothly increases a motor’s speed until its desired RPM, rather than slamming voltage into it all at once. This is a desired feature as its ability to reduce inrush current and limit peak electrical demand on motor start-up reduces mechanical stress on the system and prevents overcurrent scenarios. Source SMC Plus Soft Starters Here To achieve this, soft starters use thyristors, or...
When a plant experiences a planned shutdown, turnaround, holiday outage, or utility maintenance window, one or more PowerFlex drives fail within minutes or hours of re-energization. This is a distinct, recurrent pattern that maintenance engineers in the heavy industry can quickly identify. After years of trouble-free operation, the drive suddenly malfunctions, trips a breaker, or, in the worst situations, literally destroys an IGBT module. It is a foreseeable result of power electronics deteriorating when idle, contaminants and moisture building up when a drive isn’t producing heat, and a plant’s restart cycle interacting with both. The difference between considering every shutdown-related failure as a mystery and creating a restart strategy that stops it is an understanding of these mechanics. The internal parts of a PowerFlex drive are designed to operate continuously or almost continuously. Long-term proper operation of the DC bus electrolytic capacitors, IGBT gate driver boards...
When designing or making electrical installations, the first thoughts often turn to how much safety margin to build into the electrical design so it will withstand a certain amount of overcurrent during an emergency or surge. But when we install a VFD, the idea of putting an oversized one to build in a safety margin actually backfires. An oversized drive does not provide any safety margin — it decreases energy efficiency and motor protection while increasing harmonic distortion and costs. A good rule of thumb is that any drive should not be larger than twice the rating of the connected motor. Drive manufacturers go further and specify that the motor must carry a rating above 50% of the drive. Combining a 150 kW drive with an 11 kW motor gives only a 7.3% ratio. The issue comes from the large difference between the motor’s operating current and the VFD’s rated current range. A VFD measures the output current and uses it for motor control, torque estimation, and electronic overload...
DC Drive regen technology isn’t anything new. In fact, they’ve been around since the late 1800s and have been evolving to make industrial systems more efficient. In Rockwell Automation’s PowerFlex lineup, regeneration can be handled through several different architectures, including active front end systems, common-bus systems, regenerative DC drives, and medium-voltage regenerative drives. Today, this lineup extends its regenerative technology to the PowerFlex 755TR, PowerFlex 755TM, PowerFlex 755TL, PowerFlex 7000, PowerFlex DC , and the PowerFlex 700AFE. To understand how a PowerFlex drive handles regenerative loads, it’s best to start at the drive’s front end. In a traditional AC drive with a passive diode front end, incoming AC power is rectified into DC power before the drive inverts it back into controlled AC power for the motor. Under normal motoring operation, that power path is one-directional from the line, through the drive, and out to the motor. When the motor...
Although a PLC installed on a vibrating conveyor frame in a steel mill and a PLC sitting in a climate-controlled control room can belong to the same product family, the technical choices made for each installation are very different. Compared to traditional factory automation, industrial control systems utilized in hazardous or toxic industrial environments need to have far more robust designs and better environmental ratings. Corrosive vapors, conductive dust, explosive gases, excessive humidity, loud electrical noise, and extremely high or low temperatures can all be found in these settings. Buying a more costly processor is not the only option when designing a PLC system for these circumstances. Conformal coating, vibration mounting, thermal management, enclosure selection, EMI shielding, and hazardous area classification are all systems engineering tasks that must be completed at different stages of the design process. Understanding the particular environmental stresses the PLC...
Modern mobile machinery and modular skid systems rely on Human Machine Interface (HMI) devices for real-time visibility, reliability, and durability in rugged operating environments. Rockwell Automation PanelView operator interfaces are designed for machine-level monitoring, control, diagnostics, and visualization. When properly mounted and protected, PanelView terminals can be used on portable industrial equipment, mobile skids, and machine-mounted control stations where operators need local visibility into machine status, alarms, diagnostics, and process conditions. This allows operators to quickly understand machine status and respond to faults and process changes. PanelView Plus 7 Standard terminals are designed for easy programming and integrate with Rockwell Automation architectures. These interfaces dynamically visualize operating information, making them suitable for systems that require quick operation and troubleshooting. The PanelView Plus 7 Standard series is intended for...
Safety is the foundation of hazard-free and reliable industrial applications. DC drives operate at hazardous current and voltage levels to regulate the field current and armature voltage, thereby precisely controlling motor speed, torque, and direction. Therefore, strict adherence to established electrical safety protocols such as proper grounding, isolation, and Lockout/Tagout (LOTO) procedures, as well as compliance with IEC 61800-5-1 standards, is essential in DC drive systems. It helps isolate dangerous voltages and minimize arc flash hazards, protecting both personnel and machinery from catastrophic electrical faults. This article provides a detailed technical analysis of the essential safety considerations for designing, operating, and maintaining DC drive systems. A DC drive system is an electronic motor controller designed to regulate the torque, speed, and rotational direction of a DC motor. It achieves this by actively modulating the current and voltage applied to the...
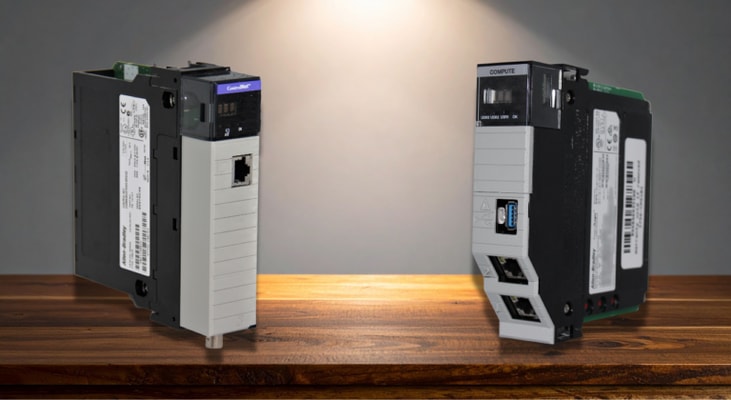
A new installation is not the same as a retrofit project. The selection logic for a ControlLogix processor must take into consideration elements that are absent from a greenfield project, and the risks and constraints are different. A processor must fit into a panel sized for a PLC-5 or SLC 500 chassis, communicate with devices never intended for EtherNet/IP, coexist with existing wiring, and be maintainable by a team that has worked on RSLogix 500 for years. A predetermined set of technical criteria must be followed to make the proper choice. That approach is covered from the start in this article. The first task on any ControlLogix retrofit is documenting the full scale of the legacy system, not just the I/O count, but everything the existing controller manages. A practical first pass is to group the 5580 processors by memory class: 1756-L81E for smaller systems, 1756-L82E or 1756-L83E for moderate retrofits, and 1756-L84E or 1756-L85E for larger PLC-5 migrations, high tag counts...
To the untrained eye, wiring a motor to an AC drive, more commonly known as a variable frequency drive, may seem like a simple job of plugging the motor in and routing the wiring to make it look clean. The length of the wires might not even be a concern, because in an ideal world with ideal resistance, it wouldn’t. The problem is that we live in a less-than-ideal world, and the rules of physics are nonnegotiable. Whether it’s traces on a PCB or wires during a motor install, the longer the connection point, the higher the resistance, heat buildup, and voltage drop. This matters more than you might expect when it comes to installing AC drives. Before getting into it, if you would like to familiarize yourself with how an AC drive works, check out this article here ! The inherent design of an AC drive is to output fast voltage pulses rather than a clean sine wave. Each time the AC drive switches, a voltage pulse travels down the motor cable to the motor. With a shorter cable, the pulse...
Choosing the right PLC is one of the most important decisions in an automation or infrastructure project. A well-designed PLC can help minimize commissioning time, reduce stability problems during long-term operation, and lower maintenance costs. In energy-intensive applications, PLCs do more than handle basic logic. They may also support energy optimization, multi-VFD coordination, system monitoring, and long-term lifecycle reliability. The system requirements should drive the PLC selection, not the brand name alone. Start by determining how many I/O points the application requires. A small machine may only need a few dozen I/O points, while a tunnel, pump station, or utility system may require hundreds or thousands across ventilation, drainage, lighting, monitoring, and safety-related equipment. In larger systems, distributed I/O, expansion capacity, remote communication, and reliable backplane or network performance become major selection factors. For applications tied into utility...
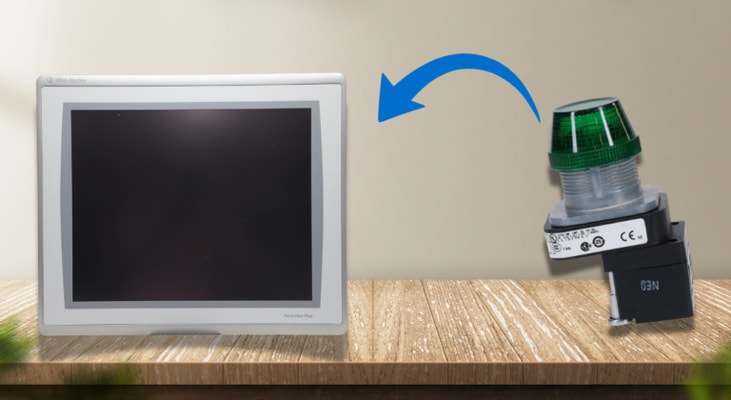
The question of whether to replace the row of pushbuttons and selector switches on the HMI eventually arises on practically every classic machine or control panel. One touchscreen rather than twenty separate devices seems like a straightforward surface-level alternative. The engineering response is far more complex. The way the operator interface is wired, how PLC logic processes inputs, how data is logged, and how alerts are displayed are some of the key changes. Everything else that comes into contact with the hardwired safety circuit must remain unchanged. The difference between a clean migration and one that results in unexplained PLC logic rewrites, or safety compliance problems mid-commissioning, is to formally distinguish between these two groups before the project begins. Before discussing what changes, it helps to be precise about what a pushbutton panel is doing at the wire level. Each pushbutton, start, stop, jog, and mode select wires a physical contact directly to a PLC...
Conveyor systems serve as crucial circulatory networks in warehouses, airports, mining operations, food processing plants, and manufacturing industries. Well-designed conveyors drastically reduce manual material handling while improving operational efficiency and ensuring consistent output quality. Allen-Bradley PowerFlex drives are essential components of modern conveyor systems, whose performance relies heavily on precise control of the connected motors. PowerFlex drives utilize advanced control modes, including Sensorless Vector Control (SVC), Volts/Hertz (V/Hz), and TotalFORCE technology (available on the PowerFlex 755T series), to deliver high-precision regulation of motor speed and torque. This highly precise motor control enables smooth acceleration and deceleration of conveyor systems, significantly reducing wear and tear on conveyor belts, gearboxes, and bearings by minimizing mechanical shock. Selecting the correct PowerFlex drive helps minimize system downtime, enhance...
Choosing the right PanelView HMI is no easy task; it’s not just about the screen size or the communication protocol. A major choice is whether a PanelView terminal will be equipped with a keypad, a touchscreen, or both. PanelView models with a keypad enable a variety of functions under harsh operating conditions that touchscreen interfaces cannot. By understanding the true costs and benefits of these input methods, engineers, operators, and maintenance personnel can select the most appropriate PanelView solution for their application. Modern PanelView families vary widely in the input options available. PanelView 5310 and 5510 terminals use touchscreen input, while PanelView 800 and legacy PanelView Plus 6 models include keypad, touchscreen, or keypad/touchscreen options depending on the model. PanelView Plus 7 Standard terminals are primarily touchscreen-based. The choice of interface affects the operator’s efficiency, navigation speed, maintenance requirements, system reliability...
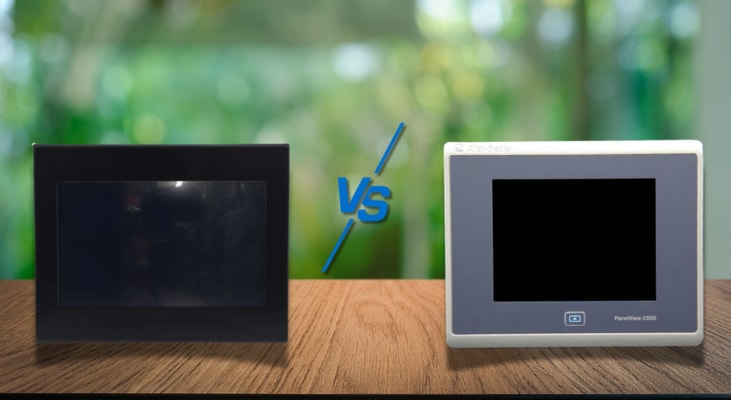
A graphic terminal remains an invaluable asset within most automated systems. It gives operators a practical way to see what a machine is doing, respond to alarms, adjust process values, and keep production moving without needing to dig through the control cabinet every time something changes. Of course, the effectiveness of the terminal varies depending on factors such as screen size, graphic design, responsiveness, and so on. Because of this, it can get a bit overwhelming trying to spec the perfect HMI for your setup. Today, we’re here to narrow down your search with two popular offerings on the market: The Mitsubishi GOT2000 series and the Allen-Bradley PanelView 5500 series. Both of which are built for a serious industrial environment, yet lean into their own strengths that we will go over to help you make a more informed decision. Before diving into the comparisons, it’s best to go over what each HMI’s family is trying to accomplish. While the Mitsubishi GOT2000 and the...